Spinning Masterbatch Brand Selection Tips for Vibrant Fibers
2026-09-20
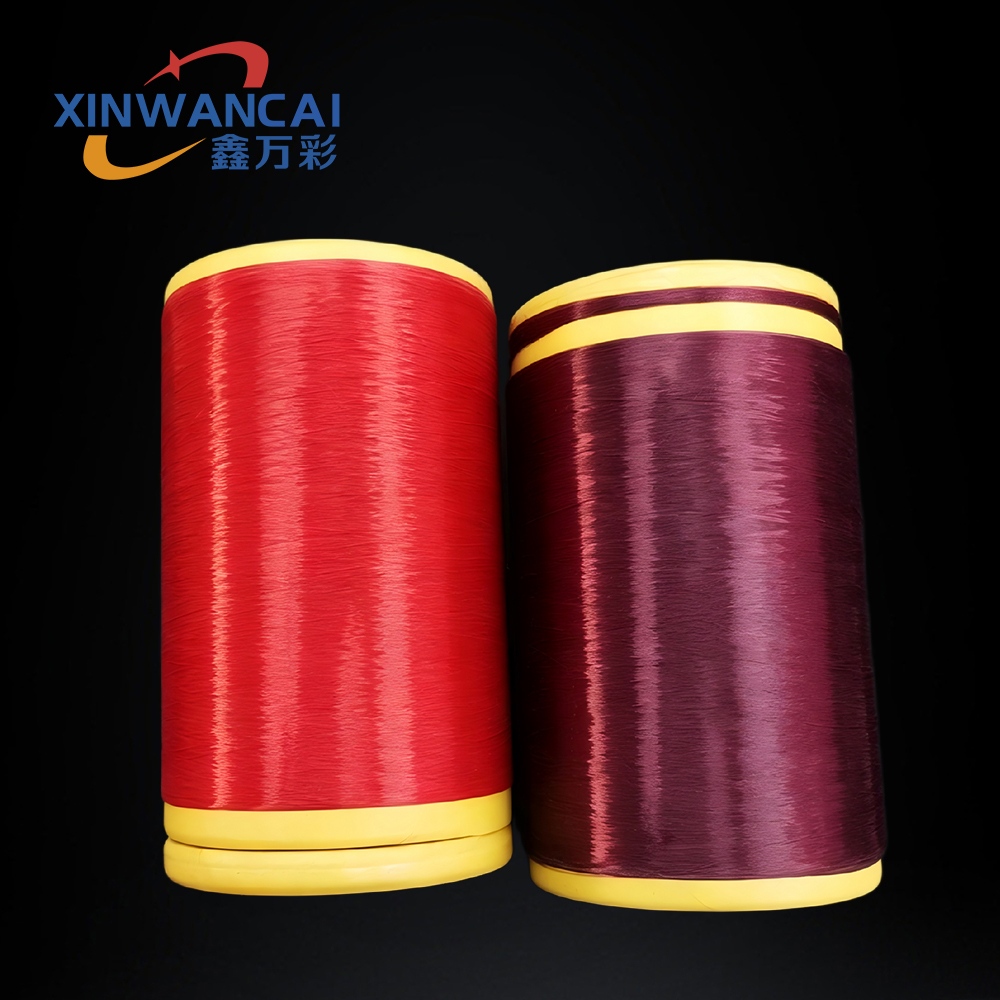
Choosing the right spinning masterbatch can feel like chasing color in a moving kaleidoscope—get it wrong, and your vibrant fibers turn dull, uneven, or worse, clog your production line. But the secret to locked-in brilliance isn’t just pigment load; it’s matching the masterbatch’s polymer base, dispersion quality, and heat stability to your exact spinning process. That’s where a specialist like Xinwancai changes the game: their fiber-grade formulations target melt-spun polypropylene, polyester, and nylon with tight particle control that survives high-speed spinning and downstream drawing. Before you burn another kilo of trial batches, let’s break down what actually separates a true spinning masterbatch from a generic color concentrate—and how to pick a brand that keeps your shades vivid from pellet to fabric.
Dispersion Quality You Can See Under a Microscope
A microscope turns a routine dispersion check into a diagnostic tool. Rather than guessing from viscosity or settling behavior, you can directly observe whether particles exist as isolated units, loose clusters, or dense agglomerates. This visual evidence reveals the true state of your dispersion in seconds.
Small aggregates that remain invisible to the naked eye become obvious under magnification. You can distinguish between soft flocs that break apart under slight shear and hard agglomerates that resist breakdown. That distinction matters because it tells you whether your formulation needs a tweak in mixing speed, a different wetting agent, or simply more time.
Color uniformity, edge sharpness, and particle distribution all speak through the lens. A well-dispersed sample shows consistent spacing and similar particle sizes, while a poor one shows streaks, clumps, or uneven density. These patterns guide formulation adjustments without waiting for long-term stability tests.
Consistency That Survives a Year of Production Runs
After the initial setup, most production lines look promising. The real challenge shows up around month three, when subtle shifts in raw materials, tool wear, and ambient conditions begin to nudge outputs away from the golden sample. A process that holds its tolerances through four quarters of continuous runs does not get there by accident. It requires a deliberate feedback loop: every batch is measured, every deviation is traced to its source, and corrective actions are locked into the standard operating procedure.
What separates genuine consistency from short-term stability is the willingness to treat drift as a design problem rather than a maintenance afterthought. Instead of chasing individual bad parts, the focus stays on tightening the inputs—supplier lot acceptance, machine warm-up cycles, calibration intervals, and operator handoff notes. Over a year, these small disciplines compound. The line that was producing good parts in January produces parts that are statistically indistinguishable in December, not because nothing changed, but because every change was understood and controlled.
For anyone relying on that output, this kind of consistency means fewer incoming inspections, less safety stock, and no awkward conversations about why the latest shipment behaves differently from the previous one. It is the quiet confidence of knowing that the hundred-thousandth unit off the line will fit, function, and fail at the same rates as the first.
Heat Stability Beyond the Data Sheet
Data sheets reduce thermal performance to a single number, but real-world heat exposure rarely works that way. Components cycle between hot and cold, soak at elevated temperatures for months, and face localized hot spots that no standardized test can fully replicate. Relying on the headline decomposition temperature or heat deflection value often misses how a material behaves when those conditions interact.
What matters more is how properties drift over time. A formulation might hold its tensile strength for the first 500 hours at 150°C, then lose stiffness rapidly as antioxidant packages deplete or filler-matrix bonds start to fail. Color shift, embrittlement, and dimensional growth can appear long before any dramatic thermal breakdown, and these subtle changes determine whether a part remains functional in service.
Rather than chasing a higher number on a spec sheet, it is worth looking at aging curves from prolonged exposure tests that mirror actual operating cycles. Tracking retention of elongation, impact resistance, and weight loss across multiple time points reveals the true thermal endurance curve—information that no single data-sheet value can provide.
Resin Compatibility Without the Guesswork
Most resin selection failures come down to assumptions about chemical exposure or surface bonding that are never validated early. Instead of treating compatibility as a shot in the dark, start with the actual service environment: list every solvent, cleaner, fuel, or plasticizer that will contact the cured resin, including trace contaminants. Then check those substances against published resistance data for the specific resin chemistry—epoxy, urethane, vinyl ester, and polyester all behave very differently when faced with even mild acids or alcohols.
After narrowing the field on paper, run small, cheap exposure tests that mimic real conditions: temperature, concentration, and contact time matter far more than a supplier’s generic rating. Soak a cured sample in each critical fluid for 24 to 72 hours, measure hardness, weight change, and visual degradation, and compare the results to a control. This step catches incompatibilities that datasheets miss, such as plasticizer migration causing softening or stress cracking from a solvent the resin was “supposed” to resist.
Finally, build a simple internal matrix that records which resin systems survived which chemical and thermal cycles in your own facility. Over time, this becomes a reliable reference that takes the guesswork out of future projects—new applications can be matched to known winners instead of starting from zero. It’s not about finding a single universal resin; it’s about knowing exactly what your chosen system can and cannot handle before you commit to production.
Technical Support That Shows Up on the Factory Floor
When a machine goes down on the factory floor, every minute of downtime ripples through production schedules, delivery promises, and the bottom line. That's why our technical support doesn't hide behind a phone line or a ticket queue. Our engineers walk the same concrete floors as your operators, carrying tools and laptops into the noise and heat of real production environments. They don't just diagnose from a distance—they stand beside the equipment, listen to the hum of motors, watch the rhythm of conveyors, and talk directly with the people who run the line every day.
This hands-on approach changes the nature of troubleshooting. Instead of relying on secondhand descriptions or grainy photos, our support team sees the problem in context—the vibration in a bearing, the lag in a sensor, the way a fixture jams under full load. Because they understand your specific process and machinery, they often spot subtle issues that remote diagnostics would miss entirely. And because they're physically present, they can test fixes immediately, adjust parameters on the spot, and verify results before the shift changes.
Beyond emergency repairs, our floor-level presence means proactive care. Regular walkthroughs let our engineers catch wear before it becomes failure, suggest small adjustments that improve throughput, and train your team on maintenance tricks that reduce recurring faults. The result is not just faster fixes when things break, but fewer breakdowns in the first place—and a support relationship built on shared workspace, not just shared screens.
Real Cost of Color Is Not the Price Tag
A can of paint might cost twenty dollars, but that number tells you almost nothing. The actual expense shows up when the color fades unevenly after one summer, when a brand's signature red shifts between screens and packaging, or when a designer spends three extra rounds matching a swatch under different lighting. Those hours and reprints add up faster than the initial pigment purchase.
There is also the environmental toll hiding behind vivid hues. Some pigments require heavy metals or complex chemical processes, and disposal of leftover mixed paints often ends up as hazardous waste. Choosing a cheaper color now can mean paying a much larger cleanup bill later, not to mention the reputational cost if customers notice inconsistency.
Then there is the psychological price. A poorly chosen color can make a product feel cheap, a room feel cramped, or an interface feel untrustworthy. Recovering from that first impression usually costs more than investing in well-tested color research from the start. The price tag only covers the material; it never covers the risk.
FAQ
Look beyond standard datasheets. Request trial runs on your exact fiber grade and monitor filter pressure rise over several hours. A brand that resists pressure buildup usually means fewer filament breaks and cleaner, more vibrant color.
Ask for a pressed film or a small-scale spin trial. View it under a light box. Even tiny pigment agglomerates will appear as dark specks. If the supplier seems reluctant to provide this, treat that as a warning sign.
Yes. A carrier with poor compatibility or a large melt flow mismatch can create micro-roughness on the fiber surface. That roughness scatters light and reduces perceived vibrancy. Insist on a carrier from the same polymer family as your base resin.
Not necessarily. Overloading can lead to poor dispersion, filter clogging, and lower fiber tenacity. Balanced formulations with optimized pigment-to-carrier ratios usually deliver deeper, cleaner shades without hurting spinability.
High-speed spinning exposes the melt to significant heat. If pigments or additives degrade, colors can shift or fade. Choose a brand known for heat-resistant pigments tested at your exact process temperature, not just generic polypropylene or polyester conditions.
Work with a supplier that uses spectrophotometric controls and keeps reference samples from each lot. Ask for a delta E guarantee, ideally below 0.5, and find out how they handle rework if a lot drifts outside the agreed range.
Usually yes, but not automatically. The real value shows up as lower reject rates, fewer spinning breaks, and less downtime. Calculate total cost per kilogram of first-quality yarn rather than comparing masterbatch price alone.
Request accelerated weathering data using your actual fiber, not just generic resin plaques. Ask about lightfastness ratings, UV stabilizer packages, and any known interactions between pigments and spin finishes.
Conclusion
When your fiber line runs around the clock, the wrong masterbatch choice shows up fast—not in a lab report, but in streaky color, clogged spinnerets, and shade drift that makes your downstream customer question every reel. Before you sign off on a brand, pull a pressed film or a fiber cross-section and look under the microscope. If pigments aren't dispersed as discrete, sub-micron particles, you'll see agglomerates that translate directly into breakage and dull color. A supplier who won't hand you a microscope slide or let you run a filter pressure test isn't worth the invoice. Equally important is consistency over time: the first batch may look brilliant, but what about the tenth run six months later? Ask for retained samples from previous production lots and measure the color difference yourself. Heat stability is another silent killer—some pigments survive the datasheet's two-minute dwell test but degrade during long extruder residence times or high-speed spinning. Request thermal aging data at your actual processing temperature and residence window, not just a generic TGA curve.
Resin compatibility is rarely as simple as “works with PP or PET.” Different catalyst residues, comonomer levels, and additive packages can shift the melt viscosity and nucleation behavior enough to ruin spinline stability. A dependable masterbatch supplier will ask about your exact resin grade, not just the polymer family, and will adjust the carrier system accordingly. Then there's the human factor: when shade goes off at 3 a.m., you need a technical partner who will send an engineer to your floor, not a voicemail. Pay attention to how they handle a trial—do they stick around for start-up, check filter pressure rise, and inspect yarn cross-sections with you? Finally, calculate the real cost of color by including yield, downtime, scrap, and added filtration. A cheap masterbatch that forces you to change screen packs twice a shift or lowers your first-quality yield by two percent is far more expensive than a higher-priced concentrate that runs clean. Choose the brand that understands fiber spinning is a continuous, unforgiving process—and proves it on your line.
Contact Us
Contact Person: JACK
Email: [email protected]
Tel/WhatsApp: 86 18650130917
Website: https://www.xinwancai.com/