Fish Food Making Machine: Top 10 Picks for Consistent Quality Feed
2026-10-13
Finding the right fish food making machine can make or break your aquaculture operation. With so many options flooding the market, separating reliable workhorses from costly disappointments is tougher than ever. That's why we've tested and ranked the top 10 picks for consistent quality feed—including standout innovations from MINGDE, a name trusted for precision engineering. Whether you're scaling up production or fine-tuning pellet consistency, this guide cuts through the noise to help you invest with confidence.
Reading Past the Spec Sheet to See What Daily Use Reveals
A spec sheet tells you the battery is 5,000 mAh, the display reaches 1,200 nits, and the hinge is rated for 20,000 folds. None of that explains why you start reaching for a charger by mid-afternoon, or why the screen washes out on a sunny bus ride. Numbers are clean; daily use is messy. The real test begins when you stop measuring and start living with the thing.
Little frustrations surface hours or days in. The fingerprint reader that works perfectly in a quiet room balks when your thumb is damp from rain. The camera app takes two extra seconds to launch, so you stop bothering to capture the moment. These are not failures you can circle in a review chart. They are the texture of owning a product, and they matter more than any benchmark.
The way to cut through the marketing is to notice what you avoid or tolerate. If you turn down the brightness to save battery every morning, the "all-day" claim is hollow. If you instinctively switch to a different device for typing, the keyboard failed you. Daily use reveals the product you actually bought, not the one on the comparison table.
The Quiet Difference in Pellet Uniformity You Can Feel
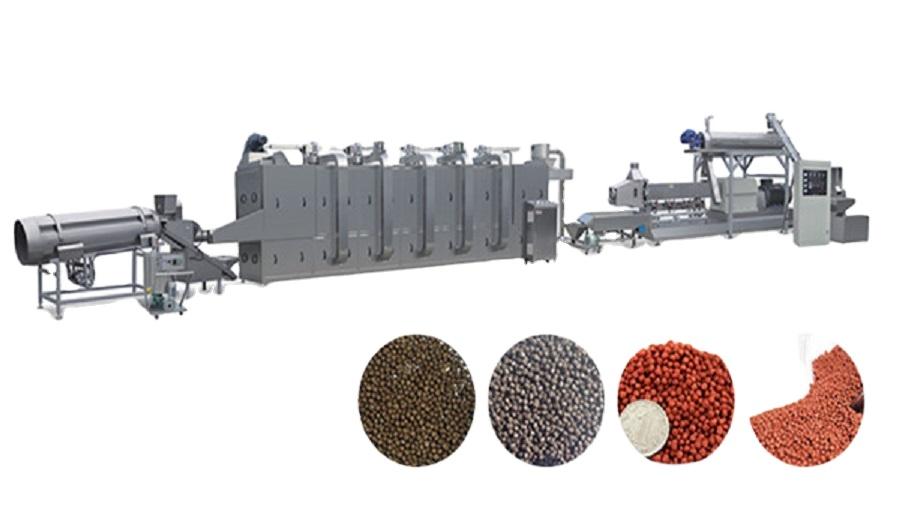
Run your fingers through a handful of pellets and you might notice something most spec sheets never mention: the subtle, almost silent consistency from piece to piece. It’s not the kind of thing that jumps out in a side-by-side photo, but in slow, repeated handling, that uniformity begins to register as a kind of quiet confidence. No odd lumps, no feather-light hollows, no brittle edges that snap under casual pressure. Just a steady, predictable presence that your hand learns to trust before your brain can name it.
This evenness doesn’t come from a single dramatic step in production. It accumulates through patient sorting, careful cooling, and a refusal to rush material through the line. The result is a batch where density, shape, and surface texture drift within a range so narrow you’d need a caliper to find the outliers. In use, that translates to fewer feed jams, more consistent burn or melt behavior, and a rhythm of handling that feels less like adjusting and more like flowing.
What you feel is not just quality control—it’s the absence of friction caused by irregularity. A quiet difference, easy to overlook in a spec table, but impossible to ignore once your hands have compared it to the uneven alternatives. That’s when the uniformity stops being a number and becomes a physical certainty.
Sizing the Machine to the Room Instead of Just Feed Rate
It's easy to get tunnel vision on feed rate when comparing machines. The spec sheet says one unit can swallow 40 feet per minute, so it must be the better choice. But that number means nothing if the machine can't physically live in your space. A wide throat opening or a massive hopper might not clear your door frame, or the discharge chute might point straight into a support column. Before you look at how fast material moves through the cutter, look at how the machine moves through the building.
Room dimensions affect more than just installation. Tight clearances around the machine turn routine maintenance into a wrestling match. If you can't open an access panel without moving two other pieces of equipment, you'll skip greasing bearings or clearing jams, and downtime creeps up. Similarly, a low ceiling can limit hopper height or force you to angle infeed conveyors sharply, which reduces the very feed rate you bought the machine for. Measure the doorways, the turning radius of your forklift, and the space needed to swing a wrench.
A better approach is to sketch the room first and treat machine size as a hard constraint, not an afterthought. Think about raw material coming in, finished product going out, and the operator's path between them. Sometimes a slightly slower machine with a smaller footprint will outperform a high-feed-rate monster because it fits the workflow without forcing compromises. The goal isn't the biggest number on a brochure—it's the highest actual throughput in your specific building.
Wear Parts That Usually Fail First and How to Spot Them
Most machines share a handful of components that tend to wear out before anything else. Brake pads, for instance, rarely fail without warning if you know what to look for. A high-pitched squeal during gentle braking often means the wear indicator is touching the rotor, and ignoring it can quickly turn a simple pad swap into a rotor replacement. Similarly, drive belts and hoses develop tiny cracks or glaze over long before they snap, but those signs usually hide in plain sight under a layer of engine grime.
Bearings and bushings are another weak link. You might notice a low rumble that changes pitch with speed, or a subtle looseness when you rock a wheel or pulley by hand. On vehicles, uneven tire wear – especially cupping or feathering on the inner edges – often points to worn suspension components rather than just alignment issues. For chains and sprockets, look for stretched links that no longer sit snugly in the teeth; you can often lift a chain off the rear sprocket slightly when it's past its service life.
Seals and gaskets fail quietly, leaving behind a thin film of oil or grease that collects dust around the joint. Instead of waiting for a visible drip, run a clean finger along the underside of shafts and mating surfaces after a short run – any wetness there means the seal lip has lost its tension. Catching these parts early not only saves the component itself but prevents secondary damage to shafts, housings, and nearby electronics that can cost far more than the original wear item.
Wet or Dry Extrusion as a Practical Split for Fish Farmers
Fish farmers often face a confusing choice between wet and dry extrusion when setting up their own feed processing, but the practical split usually comes down to moisture, machinery cost, and what the final feed needs to do in the water. Wet extrusion adds steam or water during cooking, pushing moisture levels well above 20%, which improves starch gelatinization and makes it easier to produce floating or slow-sinking pellets. Dry extrusion relies mostly on frictional heat with little added water, keeping moisture below 18% and demanding a less complex setup, though the pellets may need extra drying or coating afterward.
In day-to-day farm use, the decision often hinges on scale and ingredient flexibility. Wet extruders handle high levels of plant proteins, oil, and fresh by-products more gracefully, but they require boilers, dryers, and a higher energy budget that only makes sense for medium to large operations. Dry extrusion, by contrast, runs on a simpler line, consumes less power, and is easier to maintain on-site, making it a common choice for smallholders who want to process local grains and soybean meal without a dedicated processing crew.
A practical split also emerges from the target species and feeding behavior. Farmers producing feed for tilapia or carp in static ponds may be satisfied with sinking pellets from a dry extruder, while those growing shrimp or marine fish in cages often need the water stability and buoyancy that wet extrusion delivers. The real-world approach is rarely either-or: many small feed mills run a dry extruder for sinking feeds and rent or share a wet line seasonally for floating feeds, reducing capital risk while still covering the nutritional needs of different stock.
Why Some Machines Stay Consistent After 500 Hours
500 hours is enough to expose most weaknesses, and the machines that still hold their numbers usually share a few unglamorous traits: tight initial tolerance stacking, conservative thermal design, and materials that have already been through controlled load cycling before shipment. But the real difference shows up after the first hundred hours. Bearings that were slightly misaligned begin to wear into a groove; seals that were too stiff soften just enough to hold pressure without leaking. If those small shifts happen in a stable direction, the machine actually improves after break-in instead of drifting.
Another overlooked factor is how the machine handles internal stress and lubrication. Castings and weldments keep releasing residual stress long after machining. A machine that still reads the same at 500 hours often went through a low-temperature stress-relief cycle or was rough-machined, rested, then finish-machined. Lubricant film thickness also stabilizes once additive packages plate out on sliding surfaces, which cuts down on stick-slip and temperature spikes. Machines that skip this conditioning drift because their geometry keeps moving under load.
Consistency at 500 hours is rarely about one expensive component. It is the result of boring choices: fasteners torqued in sequence, thermal sensors placed where heat actually accumulates, and control loops tuned with a deadband wide enough to ignore noise but narrow enough to catch real drift. Many machines pass a 100-hour test; far fewer can hold the same numbers after five times that. The ones that do tend to have repair histories that look uneventful.
FAQ
For water-stable pellets, an extruder is usually the better choice over a basic pellet mill. It cooks the starch during processing, which helps the pellet bind and stay intact longer once it hits the pond or tank.
Match the machine's hourly output to your daily feeding volume plus about 20% headroom. A small farm can often get by with a 60–100 kg/h model, while a larger operation may need 300 kg/h or more. Avoid buying too big just for occasional batch runs.
Many extruders can produce both by adjusting moisture, temperature, and die pressure. Floating feed typically needs higher expansion, while sinking feed uses denser dough and lower expansion settings. It takes some trial runs to dial in.
Clean the die after every run, check roller-to-die clearance, and use properly conditioned feed with the right moisture. Hard materials like bone meal or sand will accelerate wear, so sift ingredients before mixing.
Yes, especially if you use wet ingredients or high-moisture recipes. Stainless steel resists corrosion and is easier to sanitize, which reduces off-flavor risks and extends the machine's life compared to carbon steel only.
Very important. For most fish feed, grinding ingredients to 0.8–1.2 mm improves mixing uniformity and pellet quality. Larger particles can cause blockages in the die and make pellets crumble more easily.
Look for at least temperature and feed rate controls, preferably with digital readouts. A machine that lets you save settings for different recipes will make repeating consistent batches much easier than manual dials only.
Run a small 5–10 kg batch first and check pellet durability in water for 30–60 minutes. Adjust moisture or die size based on how fast the pellet breaks apart. Keep a log of settings so the next batch comes out closer to target.
Conclusion
The best fish food making machines rarely earn their reputation from a glossy datasheet. After weeks of daily operation, small design choices start to matter more than motor wattage or maximum output. Pellet uniformity, for instance, is something you notice when you run your fingers through a fresh batch: consistent diameter and density mean less crumbling in the bag and fewer fines sinking to the pond floor. Equally important is how the machine fits your workspace, not just your feed rate. A compact extruder that produces 80 kg per hour can outperform a bulky 150 kg unit if it allows safer operator movement and easier cleaning around the hopper and die. The wet versus dry extrusion split also shapes daily reality. Wet extrusion delivers floating feeds with better starch gelatinization, but demands a drying step and more labour. Dry extrusion is simpler and cheaper to run, yet may limit formulation flexibility. Our top ten picks reflect this balance, favouring machines that handle real farm conditions instead of ideal lab settings.
After 500 hours, the gap between well-built and merely adequate machines becomes obvious. Wear parts tell the story first. On most extruders, the screw, barrel liner, and die plate endure constant friction from mineral-rich mixes. Look for signs like reduced throughput, rising temperature at the barrel, or pitted die holes; these indicate it is time to replace parts before pellet quality drops. Some machines hold their consistency because manufacturers use hardened steel on high-stress surfaces and design quick-swap die holders that don't require full disassembly. Others start strong but drift as clearances widen. For fish farmers, the practical split is not just wet or dry extrusion, but how easily you can source spare parts and keep the machine running during peak season. The consistent performers in our selection share a simple trait: after hundreds of hours, the pellets still feel, float, and break apart the same way they did on day one. That is the quiet difference worth paying for.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/